Product Overview
- Sourced directly from reliable agricultural supply chains utilizing non-GMO fresh potatoes
- Optimized specifically for large-scale procurement and high-efficiency manufacturing
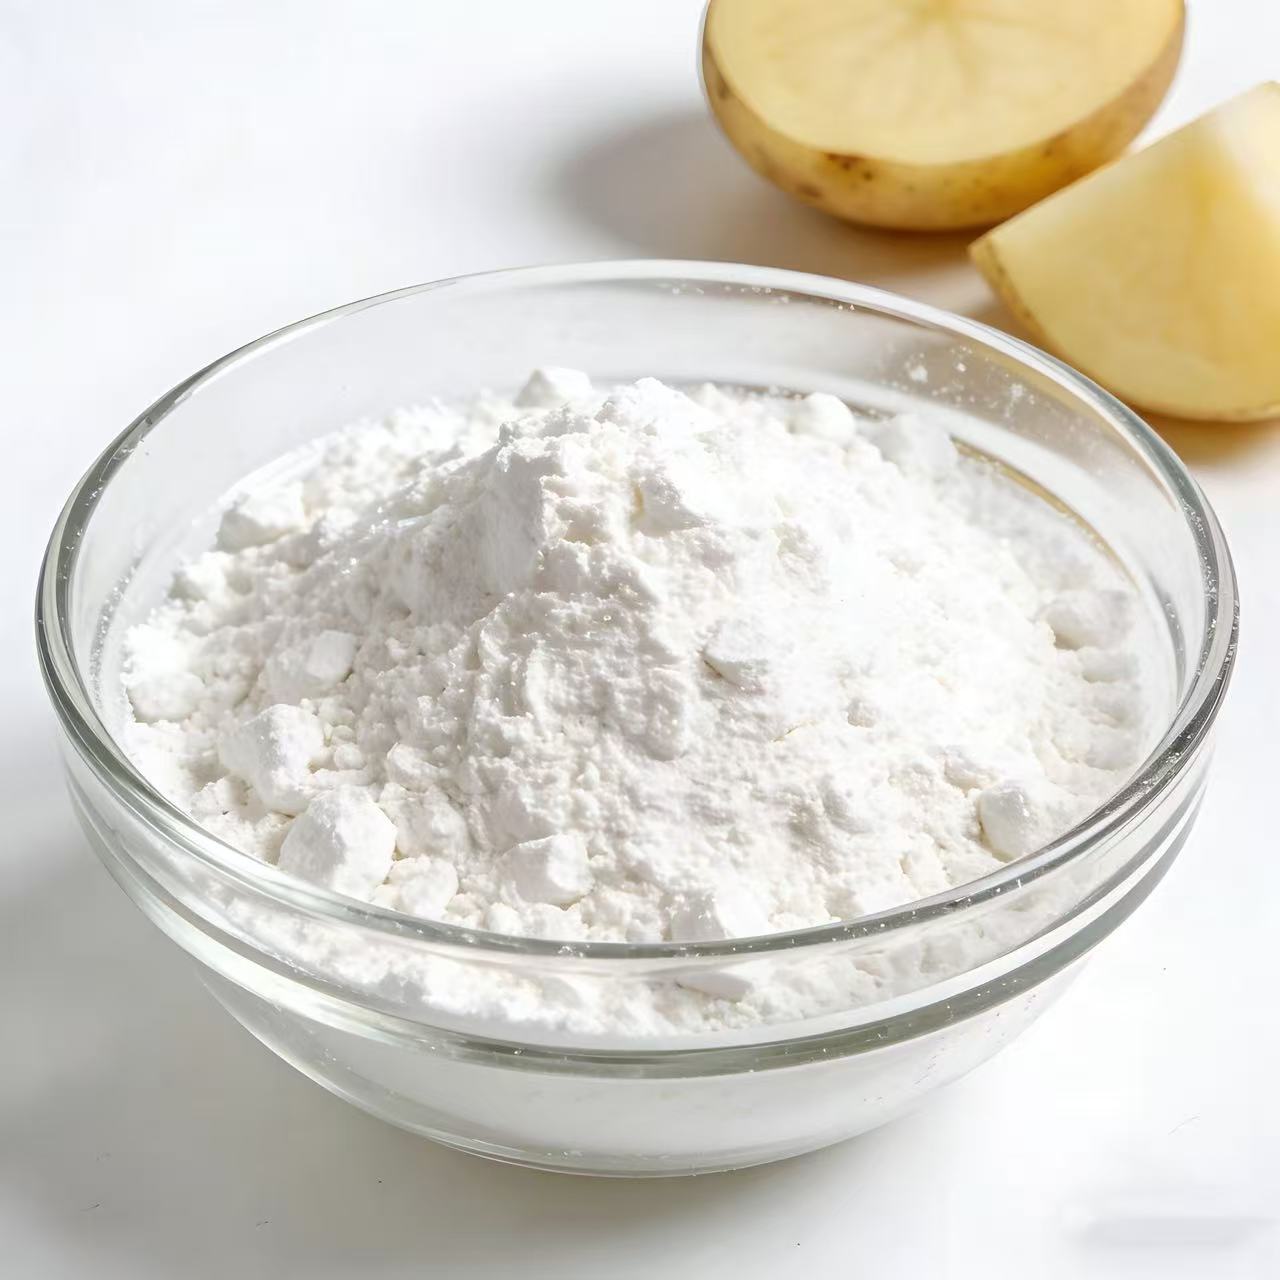
- Delivers a completely neutral flavor profile with an ultra-fine, brilliant white powder texture
- Fully compliant with stringent global food safety standards for seamless international integration
Product Description
Experience the remarkable consistency and performance of our premium low-moisture storage starch, meticulously crafted to elevate your manufacturing processes. When you examine this ultra-fine, brilliant white powder, you will immediately notice its silky, uniform texture, which guarantees seamless dispersion without clumping during high-speed mixing. Odorless and completely neutral in taste, it acts as the perfect invisible enhancer for your formulations, ensuring that the delicate, authentic flavors of your culinary or industrial creations remain entirely uncompromised. Upon hydration, it transforms into a crystal-clear, glossy paste that imparts a luxurious, smooth mouthfeel to sauces, soups, and confectionery items. Beyond its visual and tactile appeal, this high-purity starch solves critical production challenges by offering extraordinary thermal stability and freeze-thaw resilience. Whether your products face the extreme heat of industrial baking or the deep freeze of cold-chain logistics, this starch actively locks in moisture, prevents structural breakdown, and significantly extends shelf life. By integrating this high-performance ingredient into your production line, you not only enhance the sensory attributes of your end products but also optimize yield, reduce raw material waste, and streamline your entire manufacturing workflow.
Product Specifications
The following technical parameters outline the exact physical, chemical, and hygienic standards of our premium storage starch. These meticulous specifications are guaranteed through our state-of-the-art testing facilities, ensuring that every batch meets the rigorous demands of global manufacturing operations. From peak viscosity to microbiological safety, these metrics provide procurement teams and formulation engineers with the precise data required for seamless integration into complex production lines.
SPECIFICATIONS---Com Starch | Items | Standards | Unit |
| Sense | Color | white |
| Sense | Smell | neutral |
| Sense | Taste | neutral |
| Sense | Impurity | neutral |
| Physical Chemical | Moisture content | 18.9(%) |
| Physical Chemical | Ph | 6.5 ppm |
| Physical Chemical | Speck | 0.0(no./cm) |
| Physical Chemical | Protein | 0.06(%) |
| Physical Chemical | Conductivity rate | 43(%) |
| Physical Chemical | Whiteness | 92.7(%) |
| Physical Chemical | Ash content | 0.13(at 4% dry,700cmg/BU) |
| Physical Chemical | Sieve | 99.8(mg/kg) |
| Physical Chemical | Peak viscosity | 1310(mg/kg) |
| Hygiene | S02 | 0(mg/kg) |
| Hygiene | Arsenic | 0(CFU/g) |
| Hygiene | Lead | 0.05(CFU/g) |
| Expiry Packagin | Total aerobic mes.count | 2600 |
| Expiry Packagin | Yeasts& Moulds | 10 |
| Expiry Packagin | Mfing date | +36 months |
| Expiry Packagin | Paper plastic bag | |
Key Features & Highlights
Engineered for excellence, our storage starch provides a multitude of functional advantages that directly translate into improved product quality and operational efficiency for your business. From its exceptional binding capabilities to its robust environmental resistance, every characteristic is designed to solve complex formulation challenges.
- Exceptional Paste Clarity: Achieves over 90% light transmittance, giving sauces, gravies, and fruit fillings a highly desirable, glossy, and appetizing appearance.
- Superior Water Retention: Effectively traps moisture within meat products and baked goods, preventing drying out and aging during prolonged storage periods.
- High-Viscosity Performance: Reaches a peak viscosity exceeding 1000 BU, allowing you to achieve the desired thickness with significantly lower dosage rates, thereby reducing overall material costs.
- Anti-Retrogradation Properties: Maintains a smooth, non-grainy texture over time, preventing the separation of liquids and solids in soups and condiments.
- Clean Label Ready: Completely free from artificial additives and preservatives, enabling you to meet the growing consumer demand for natural, transparent ingredient lists.
Raw Material & Purity
The foundation of any superior product lies in its source materials. We exclusively utilize 100% natural, non-GMO fresh potatoes cultivated in nutrient-rich soils. By starting with the highest quality crops, we ensure a pristine base for our extraction process.
- Uncompromising Purity: Boasting a starch content of over 99%, delivering concentrated functional power for your formulations.
- Advanced Purification: Subjected to a rigorous 8-step refinement process that meticulously removes impurities, resulting in a brilliantly white, flawless powder.
- Zero Contaminants: Strictly controlled to be free from heavy metals, artificial additives, and preservatives, guaranteeing absolute safety for end consumers.
- Authentic Flavor Preservation: The completely neutral taste and odor profile ensures that the delicate, original flavors of your end products shine through without any chemical interference.
Core Physical & Chemical Properties
Our starch is chemically and physically optimized to withstand the most demanding manufacturing environments. It provides reliable structural integrity, ensuring your products maintain their intended form from the factory floor to the consumer's table.
- Extreme Temperature Resilience: Maintains stable texture and viscosity across a massive temperature gradient, from deep-freeze conditions of -40°C to high-heat baking at 120°C.
- Outstanding Freeze-Thaw Stability: Actively inhibits the formation of ice crystals in frozen foods, preserving the delicate cellular structure of dumplings, meatballs, and ice creams upon thawing.
- Efficient Thickening Power: The ultra-high peak viscosity (typically 1310 BU) means less product is required to achieve maximum thickening, optimizing your formulation economics.
- Brilliant Transparency: Creates a visually stunning, clear gel that enhances the premium look of fruit preparations, clear soups, and confectioneries.
Multi-Industry Versatility
Adaptability is a hallmark of our premium starch. Its fine, uniform particle size guarantees rapid dispersion and seamless integration, making it an indispensable asset across a wide spectrum of industrial and culinary sectors.
- Culinary and Food Processing: Acts as an elite binder and texture improver in noodles, creating a chewy, boil-resistant bite. In processed meats, it drastically boosts juiciness and overall yield.
- Paper Manufacturing: Serves as a high-performance surface sizing agent, significantly enhancing paper strength, smoothness, and printability for premium paper goods.
- Textile Industry: Functions as a reliable sizing agent and printing paste, fortifying yarn strength to reduce breakage during high-speed weaving processes.
- Pharmaceutical and Petrochemical: Delivers rapid disintegration properties for pharmaceutical tablets and acts as a crucial fluid loss reducer in complex oil drilling muds.
Strict Quality Control & Certification
Trust is built on consistency and safety. We operate an advanced, intelligent automatic cyclone production line that eliminates human error and guarantees absolute uniformity across every single batch we produce.
- Comprehensive Traceability: Our full-chain quality management system tracks every step, from the planting of raw potatoes to the final delivery of packaged goods.
- Rigorous Testing Protocols: Every batch is subjected to over 20 stringent indicator tests, including precise measurements for whiteness (≥92.7%), ash content, and microbial safety.
- Global Safety Compliance: Fully certified under internationally recognized standards including FSSC 22000, HALAL, and KOSHER, ensuring seamless integration into global supply chains.
- Hygienic Manufacturing: Produced in a state-of-the-art facility that strictly controls environmental factors to prevent any cross-contamination.
Capacity & Global Delivery
As a leading supplier, we understand that supply chain reliability is just as critical as product quality. Our massive production infrastructure is built to support continuous, large-scale manufacturing operations worldwide.
- Massive Annual Output: With a production capacity ranging from 20,000 to 50,000 tons annually, we guarantee uninterrupted supply even during peak demand seasons.
- Flexible Packaging Solutions: Choose from 25kg moisture-proof woven or kraft paper bags for easy handling, or opt for 1-ton bulk bags for maximum efficiency in large-scale operations.
- Versatile Logistics: We support a variety of shipping terms including FOB, CIF, and CFR, tailoring the delivery process to fit your specific operational requirements.
- Proven Global Reach: Successfully exporting to over 10 countries, including Russia, the USA, Canada, and New Zealand, with a track record of punctual, secure deliveries.

Customization & Technical Support
We are not just a supplier; we are your dedicated innovation partner. Our technical expertise allows us to move beyond standard offerings to create specialized solutions that address your unique manufacturing hurdles.
- Tailored Modifications: Capable of developing custom modified starch variants specifically engineered for extreme cold resistance, high acidity tolerance, or high-shear environments.
- Expert R&D Collaboration: Our professional research and development team works directly with your engineers to optimize existing formulas and develop new, cutting-edge products.
- Comprehensive Application Testing: We conduct rigorous pre-shipment testing in simulated manufacturing environments to ensure the starch performs exactly as required in your specific application.
- Cost Optimization Strategies: By fine-tuning the starch properties to your exact needs, we help you reduce raw material waste, lower production costs, and improve overall profitability.
Why Choose Us
Partnering with us means securing a competitive advantage in your industry. We combine decades of extraction expertise with cutting-edge technology to deliver a product that consistently exceeds expectations. Our commitment to your success goes far beyond the transaction.
- Unwavering Consistency: Our automated processes ensure that the first batch you receive is identical to the hundredth, eliminating the need for constant formulation adjustments on your end.
- Scalable Partnership: Whether you are scaling up a new product line or maintaining massive global distribution, our infrastructure grows seamlessly with your demands.
- Dedicated Account Management: Experience clear communication with our expert support team, ready to assist with logistics, technical inquiries, and custom development.
- Sustainable Practices: We prioritize environmentally responsible sourcing and manufacturing methods, helping you meet your corporate sustainability and ethical sourcing goals.
Frequently Asked Questions (FAQ)
To assist our procurement partners and technical engineers, we have compiled detailed answers to the most common inquiries regarding our premium storage starch capabilities and specifications.
What makes this low-moisture starch superior for long-term storage?
By strictly controlling the moisture content to below 18% (typically around 18.9% in specific testing environments) and ensuring an ultra-low microbial count, this starch naturally resists caking, degradation, and spoilage. This guarantees a highly stable 36-month shelf life under proper warehousing conditions, minimizing inventory loss.
Can the packaging be customized for automated factory lines?
Absolutely. While our standard offering is the 25kg moisture-proof woven or kraft paper bag, we frequently supply 1-ton bulk bags specifically designed to integrate seamlessly with automated silo and hopper systems in large-scale manufacturing facilities.
How does the high peak viscosity impact formulation costs?
With a peak viscosity exceeding 1000 BU (typically 1310 BU), our starch delivers immense thickening power. This allows formulators to use a significantly lower percentage of starch compared to standard alternatives, effectively reducing the overall cost of raw materials per batch without sacrificing texture.
Is this starch suitable for highly acidic food applications?
Our standard refined potato starch performs exceptionally well in neutral to mildly acidic environments (pH 6.5). However, for highly acidic applications like fruit fillings or robust sauces, our R&D team can provide custom acid-resistant modified starch solutions tailored to your exact pH requirements.
What documentation is provided with large-scale shipments?
Every shipment is accompanied by a comprehensive Certificate of Analysis (COA) detailing the specific test results for that batch, including moisture, whiteness, and microbiological data. Additionally, we provide full FSSC 22000, HALAL, and KOSHER certification documentation to support your regulatory compliance needs.


